
The right project begins with containment and cleaning acceptance. It then determines whether high-volume blower air can perform the task, or whether targeted compressed air, vacuum extraction, washing or mechanical handling remains necessary.
Quick Answer
Use a blower for CNC cleaning when the task needs continuous, relatively high-volume air to remove loose chips or surface coolant within a guarded enclosure. Define chip material and size, part geometry, coolant, nozzle arrangement, cycle time and the required result. Check airflow and pressure together at the installed duty and test the most difficult normal part.
Do not use open blow-off where chips, mist or debris can endanger people or spread contamination. A blower is not a chip collector, mist extractor or substitute for safe guarding. Heavy or trapped chips may still require a focused high-pressure jet or another removal method.
Define the Material to Be Removed
Record workpiece material and the form of the waste. Fine aluminium chips, long steel swarf, abrasive dust and wet cast-iron fines behave differently. Note whether chips are loose, packed in a bore, magnetically held, attached by viscous coolant or trapped behind a feature.
Define the acceptable end condition. Does the part need to be free of loose visible chips, dry enough for a label, ready for vision inspection, or clean to a controlled manufacturing standard? A vague request for “clean parts” encourages oversizing and makes trials subjective.
Some contamination should not be blown. Hazardous dust, combustible material and sharp swarf require risk assessment and suitable collection. Consult the machine, coolant and material safety information.
Choose the Removal Method Before the Blower
Blower air works best when it can push material toward an open, captured path. If chips sit in deep blind holes, a general air knife may pass over them. Reorienting the part, adding drainage, rotating a fixture or using a dedicated lance can be more effective than increasing total airflow.
Consider a staged process:
- allow bulk coolant to drain or use mechanical separation;
- direct chips toward a guarded collection point;
- use targeted air for recesses; and
- use a broad air knife for final surface clearing or drying.
This reduces air demand and limits recirculation. Blowing chips from one face onto another is not cleaning.
Establish Nozzle and Air-Knife Demand
Document every nozzle or knife that operates simultaneously. Record slot or orifice dimensions, working distance, angle, branch size and open time. For indexed stations, distinguish continuous flow from short pulses.
Obtain consumption data at the required nozzle pressure where possible. Add the flows of simultaneous outlets and calculate loss through the inlet filter, duct, hose, bends, valves and manifold.
A low-pressure blower and a compressed-air nozzle have different operating ranges. A small high-pressure orifice may be too restrictive for blower air. Converting the source may require larger nozzles or a blower-specific knife. Do not connect the blower to an existing compressed-air circuit and assume equal cleaning force.
Match Pressure and Airflow Together
The air system settles at the intersection of the blower curve and system resistance. Maximum airflow is normally quoted near low resistance; maximum pressure occurs at another endpoint. These two maxima are not delivered simultaneously.
Plot the required duty on the exact model curve. Check the normal part, the most difficult normal part and any reduced-output mode. Confirm that the point lies within the permitted region with reasonable margin for filter loading and production variation.
For a retrofit, measure current nozzle or manifold pressure, air consumption where possible, cycle time and accepted result. If the existing source is compressed air, compare the useful task rather than trying to match its header pressure with a blower.
Contain Chips, Coolant and Mist
Design the blow-off station as an enclosure. Guards should prevent ejected chips and liquid from reaching operators, aisles or adjacent equipment. Collection surfaces and drains should move material away so the air stream cannot pick it up again.
High-volume air can increase coolant mist. Review ventilation and mist extraction with the responsible safety engineer. A clean-air supply blower should not be treated as the extractor unless the equipment is specifically designed for the contaminated stream.
Interlock access doors where required. Validate the safe condition during jams, part removal and maintenance. Noise assessment should cover the complete nozzle and enclosure system, not only the blower’s catalogue value.
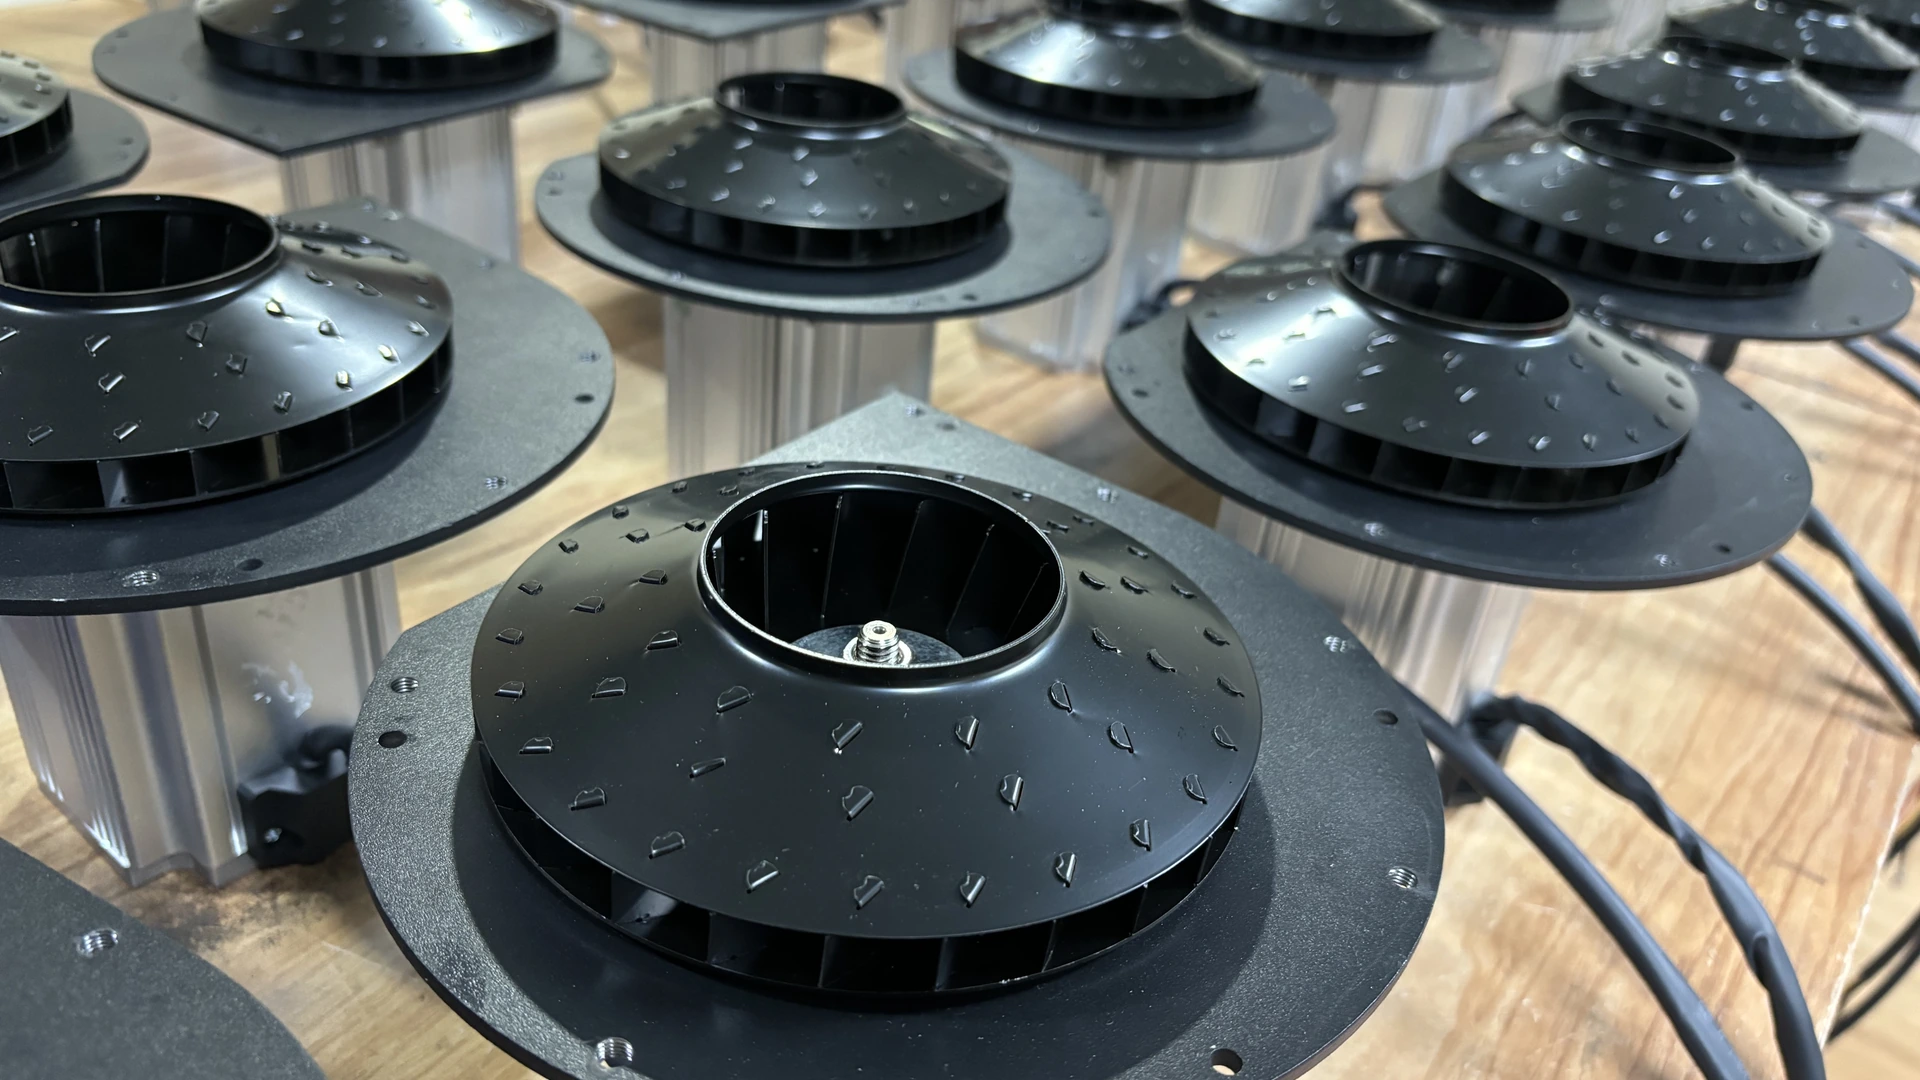
Towwind Product Range for Screening
Request the released exact-model curve, installation drawing and environmental data. Verify the clean-air duty for the selected nozzle arrangement and confirm chip containment and accepted cleaning in a guarded trial.
Confirm the selected model’s control range, electrical supply, environmental rating, certification, noise and dimensions from current released documentation. Adjustable output does not replace a verified pressure-flow match.
For a clean-air duty, confirm the released exact-model curve at the required point. If chip removal needs pressure beyond verified capability, do not force a model into the application.
Protect the Blower from Coolant and Chips
Position the inlet where it draws suitable air, away from chip spray and coolant mist. Provide filtration appropriate to the environment and enough access for frequent inspection. Never allow loose chips to enter the blower.
Route the outlet so coolant cannot drain back during shutdown or cleaning. Use engineered slope, drains and backflow protection as required; verify the exact model’s environmental rating before exposure to washdown or coolant.
Support ductwork independently and use a suitable flexible connector. Metal chips can damage soft hoses, so protect exposed lines and select materials for coolant contact where relevant.
Control the Air Around the Machine Cycle
Continuous full-output air is rarely needed while no part is present. Integrate the blower with the cell sequence using validated production, standby and stop states. Account for start and ramp time so the first part receives full required air.
Different parts may need different settings or active outlets. Store approved recipes and prevent untracked changes. During a door-open condition, jam or robot fault, the safe air state must follow the machine risk assessment.
If brief targeted pulses remain necessary, a hybrid system can use blower air for broad cleaning and compressed air only for difficult features. Measure both utilities when calculating total energy.
Compare Blower and Compressed-Air Energy Correctly
Compressed-air blow-off draws energy from the central compressor, dryer and distribution network. The local nozzle has no motor nameplate, so its operating cost can be overlooked. Measure air consumption and use a site-specific energy intensity for delivered compressed air.
For the blower, measure complete package input, including controller losses. Compare both arrangements on the same part, cycle time and cleaning acceptance. Include intermittent controls and standby operation.
For CNC cleaning, compare the complete energy boundary only after both methods meet the same chip-removal, guarding and cycle-time requirements. Include any retained compressed-air pulses; the old source, duty and schedule determine the site-specific result.
Maintenance and Diagnostic Baseline
At commissioning, record the part and cycle, active nozzles, blower command, pressure, electrical input, filter condition and accepted result. Photograph nozzle positions and valve states.
Inspect filters, hoses, clamps, guards, drains and nozzle openings on a defined schedule. A blocked nozzle can shift flow to another branch; a leak may reduce cleaning while the motor appears normal. Coolant residue can change slot geometry.
Machining environments may require early filter inspection based on mist, dust, pressure trend and the delivered manual.
Buyer and Trial Checklist
Provide the supplier with:
- part drawings or photographs and critical cleaning areas;
- chip material, form, size and coolant condition;
- cycle time and production hours;
- nozzle or knife geometry and simultaneous outlets;
- duct, hose and manifold layout;
- required pressure-flow point or existing measurements;
- guarding, drainage and mist-control arrangement;
- voltage, control and alarm interface;
- available space and service access; and
- an objective cleaning acceptance test.
Trial the hardest normal part through repeated cycles. Inspect blind holes and protected faces, not only the open surface. Record energy, noise, chip containment, mist and part result after stable operation.
Final Recommendation
An energy saving blower can be a practical replacement for broad, continuous compressed-air blow-off when loose chips and coolant can be removed at low pressure within a guarded station. It is not a universal solution for packed swarf, hazardous dust or high-pressure point cleaning.
Send Towwind the part, chip, nozzle, operating-point, control and environment data. A responsible selection should state which features the blower can clean, which may need a hybrid method and how acceptance will be proven. That makes the energy claim credible and keeps safety ahead of rated power.
Frequently Asked Questions
Can a blower replace every compressed-air chip nozzle?
No. Small nozzles and trapped chips may require higher pressure. A conversion often needs redesigned outlets, and some features may retain targeted compressed air.
Can the blower carry chips through itself?
No. Treat it as a clean-air supply unless specifically engineered otherwise. Keep chips and coolant out of the inlet and use separate collection.
Why is guarding important for air blow-off?
Air can accelerate sharp chips and spread coolant mist. A guarded, drained and assessed enclosure protects people and prevents recontamination.
How should compressed-air savings be calculated?
Measure air consumption and apply the site’s verified energy per delivered air volume. Compare with measured complete blower input at the same part, cycle and cleaning result.
What should be recorded at commissioning?
Record part and cycle, nozzle arrangement, pressure, blower setting, power, filter state, noise, containment and the accepted cleaning result.