
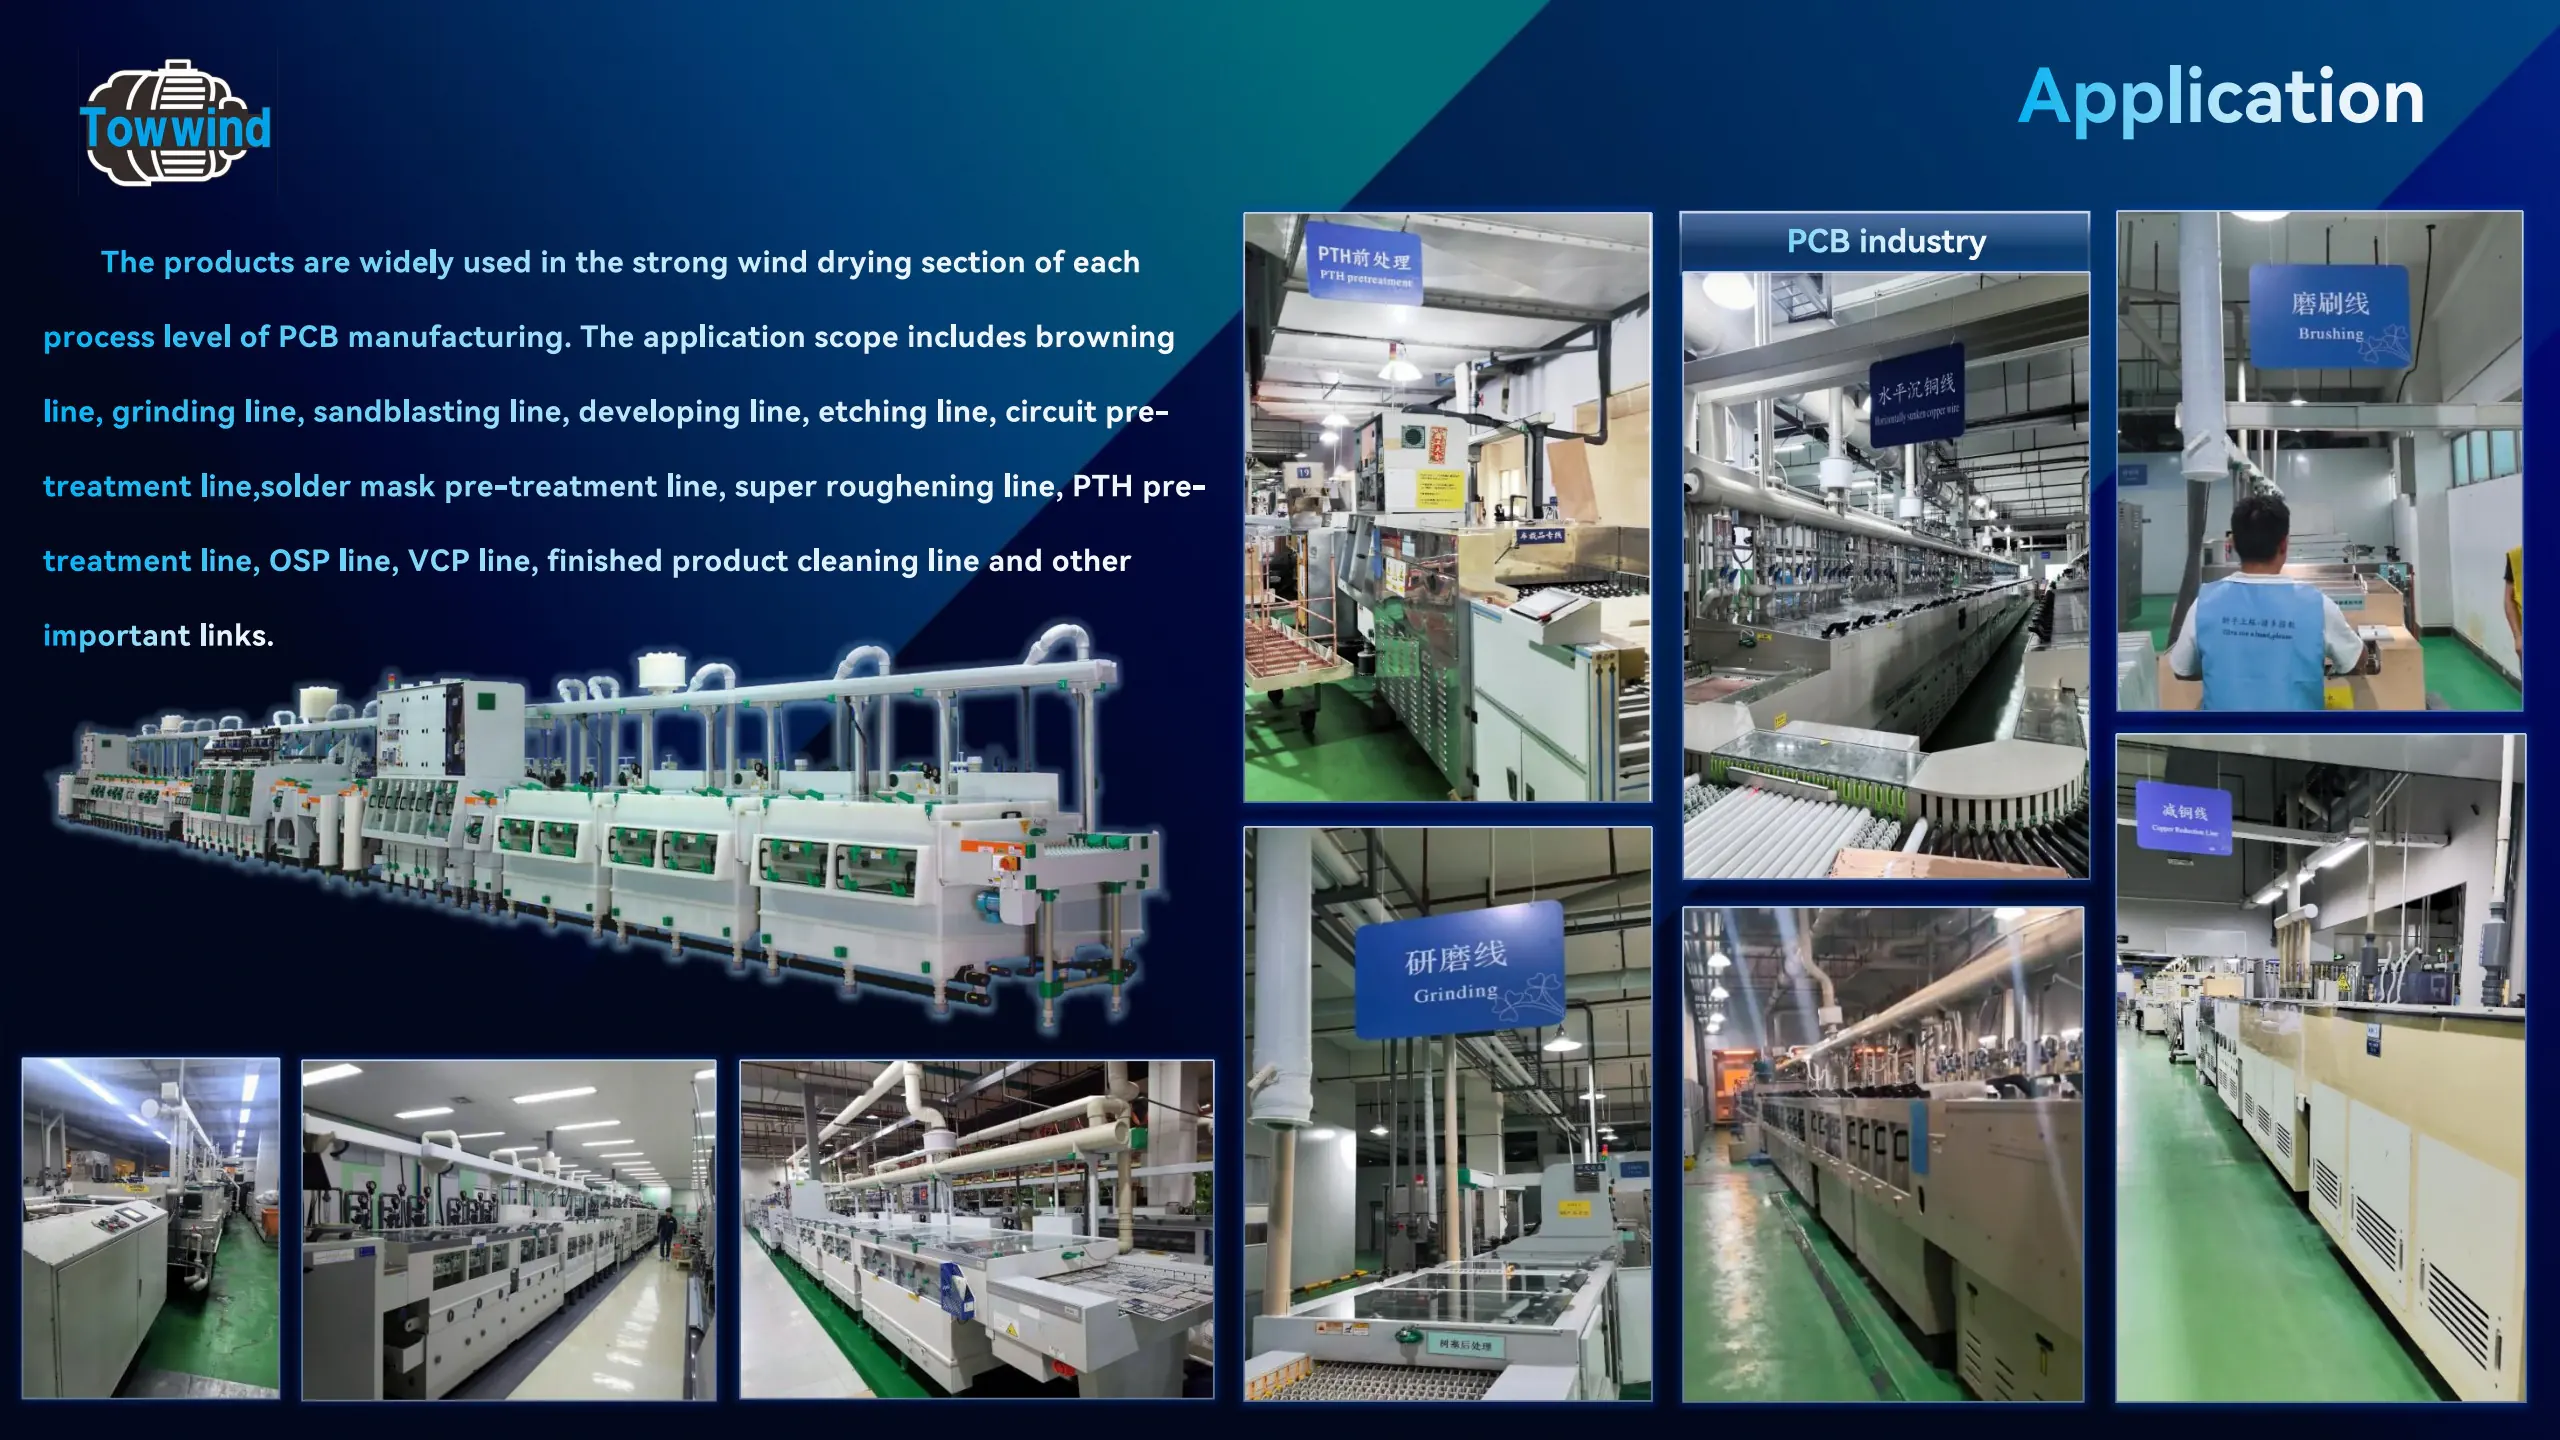
Sizing a blower for a PCB cleaning and drying line begins with the air the boards actually need, not the largest airflow printed in a catalogue. The useful result is an operating point: a required flow at the pressure imposed by the complete air path, for each production mode that must dry acceptably.
This guide is for an equipment-design engineer who needs to turn board and nozzle data into a defensible duty before comparing candidate blower curves. It is a calculation and measurement workflow, not a supplier RFQ or acceptance checklist. Where an input has not been measured or documented, leave it open rather than assigning a convenient number.
Quick answer: what data do you need to size the PCB drying blower?
Define the dryer-exit result, the PCB and conveyor modes that must achieve it, the number and geometry of the air-delivery devices, and the resistance from blower inlet to discharge. Determine airflow at the air knives or nozzles and total system pressure at that same flow. Then compare those paired requirements with model-specific performance data. A free-air maximum flow and a separate maximum pressure are not one operating point.
| Sizing input | What to record | Evidence or status |
|---|---|---|
| Dryer-exit objective | Acceptable condition for relevant board surfaces, edges, holes and features | Process requirement or trial observation |
| Production cases | PCB range, orientation, working width, normal and demanding line modes | Machine drawing and operating data |
| Air delivery | Knife/nozzle count, slot or orifice details, positions, branches and intended pressure | Device data or measurement; otherwise unknown |
| System boundary | Filters, pipe lengths and sizes, fittings, manifolds, air-delivery devices and pressure-tap locations | As-built layout or design estimate |
| Candidate comparison | Flow and pressure on the same curve, at the stated speed and conditions | Exact-model performance information |
Define the dryer-exit result and the design cases
Describe what the next process will accept, rather than writing only “dry board.” Water remaining at an edge or in a hole may matter even when a flat surface looks dry. Record which board designs, orientations and process modes are actually required; do not enlarge the duty with an undefined theoretical worst case.
For each case, record conveyor speed, board spacing, usable width, board position and the distance through the drying zone. Faster travel reduces exposure under a given air knife, but it does not justify multiplying blower capacity by speed. Geometry, air direction and the number of stages can change removal effectiveness. A demanding board at a particular speed should be identified by process evidence, not by assumption alone.
Map the air knives, nozzles and branches
Sketch the path from the blower outlet to every discharge device. Show the working width, rail obstruction, knife length, nozzle position, slot gap, stand-off and angle. Note whether branches share a manifold and whether their lengths or restrictions differ. This map identifies where air is delivered and where pressure can be lost.
Uneven branch delivery can leave PCB edges wet while the centre dries. That pattern is a reason to inspect coverage and distribution before increasing total flow. Record the layout as it will run, including adjustable rails or different board widths; a single overall pipe diameter does not describe the branch arrangement.
Determine airflow at the delivery points
Use measured process data or the air-knife/nozzle maker’s flow-versus-inlet-pressure information at the proposed setting. For parallel devices, establish the demand of each branch at its actual supply condition, then determine the combined blower requirement with any documented leakage or bypass. Do not simply multiply slot area by an assumed velocity: discharge behaviour also depends on internal geometry and pressure, and branches may not operate identically.
If discharge information is unavailable, mark the required flow as unconfirmed. A trial, a device performance curve, or a measurement on a comparable verified arrangement is needed before final sizing. The choice of measurement method and its limitations should be recorded with the value.
Determine system pressure at the same airflow
Define the pressure boundary first. Is the duty stated between blower inlet and outlet, at a manifold, or at the nozzle inlet? These are different locations. At each candidate flow, account for the relevant filter, pipe, bend, reducer, valve, manifold and air-delivery losses along the applicable path. State which losses are measured, calculated from component information, or still unknown, and do not count the same nozzle loss twice.
On an existing machine, pressure readings at identified taps can reveal whether a loss lies upstream or downstream of the manifold. Record filter condition, valve position, operating speed and active branches with the readings. On a new design, use the planned geometry and component data for an estimate; do not present that estimate as a measured machine result.
Find the operating point, not two catalogue maxima
Plot or tabulate the system’s required pressure against flow for the relevant configuration. Compare it with the candidate blower’s model-specific pressure-flow curve at the applicable speed and conditions. The intersection is the expected operating region; check that it supplies the required delivery-point flow in each required production case. A quoted maximum pressure at nearly zero flow cannot be paired with a free-air maximum flow.
If control will change speed between recipes, repeat the comparison for the normal and demanding modes, including any documented minimum usable operating range. Distinguish a proposed operating point from a validated one: nozzle data, filter loading, leakage or site conditions may shift the final result.
Compare candidates under equivalent operating conditions
Only compare electrical input or efficiency after the alternatives meet the same drying objective at the same stated air duty. Motor nameplate rating alone does not establish operating power. If the existing blower is a replacement candidate, record its measured flow, pressure, input and process result under the relevant mode; otherwise describe the comparison as provisional. No universal percentage saving or model suitability can be inferred from this worksheet.
Use a sizing worksheet with explicit hold points
| Worksheet field | Entry to complete before selection |
|---|---|
| Board and mode | Product range, orientation, width, conveyor speed and required dryer-exit condition |
| Delivery devices | Count, position, gap, branch allocation and flow/pressure source for each device |
| Air path | Filter and pipe configuration, component losses, measurement boundary and uncertainty |
| Required duty | Flow at the delivery points and total pressure at that same flow; mark missing values TBD |
| Candidate evidence | Exact-model curve conditions, predicted operating point and control modes |
Do not close the sizing calculation if nozzle performance, the as-built pipe path or the required dryer-exit result is still unknown. Identify the next measurement or document needed and who will supply it. The output of this article is a qualified duty basis; the separate supplier brief should use that basis when requesting quotation and acceptance evidence.
PCB blower sizing questions
Does a faster PCB cleaning line always need a larger blower?
No. Higher speed shortens exposure, but nozzle coverage, angle and staging also affect drying. Recheck the process result and air demand for that mode before changing blower duty.
Can I size the blower from total air-knife slot area?
Not reliably. Slot area alone does not establish the flow-pressure behaviour of the delivery devices or the losses between blower and board. Obtain device data or measured performance at the relevant pressure.
Why can PCB edges remain wet when the centre is dry?
Possible causes include rail obstruction, insufficient knife coverage or unbalanced branches. Map the distribution and record observations across the working width before treating the symptom as an overall blower-capacity shortfall.
What should I send for an operating-point review?
Send the completed duty worksheet, nozzle or air-knife data, air-path sketch, defined production modes and any measured flow and pressure with tap locations. Towwind can then review a candidate against the documented operating point; missing values remain open until verified.