
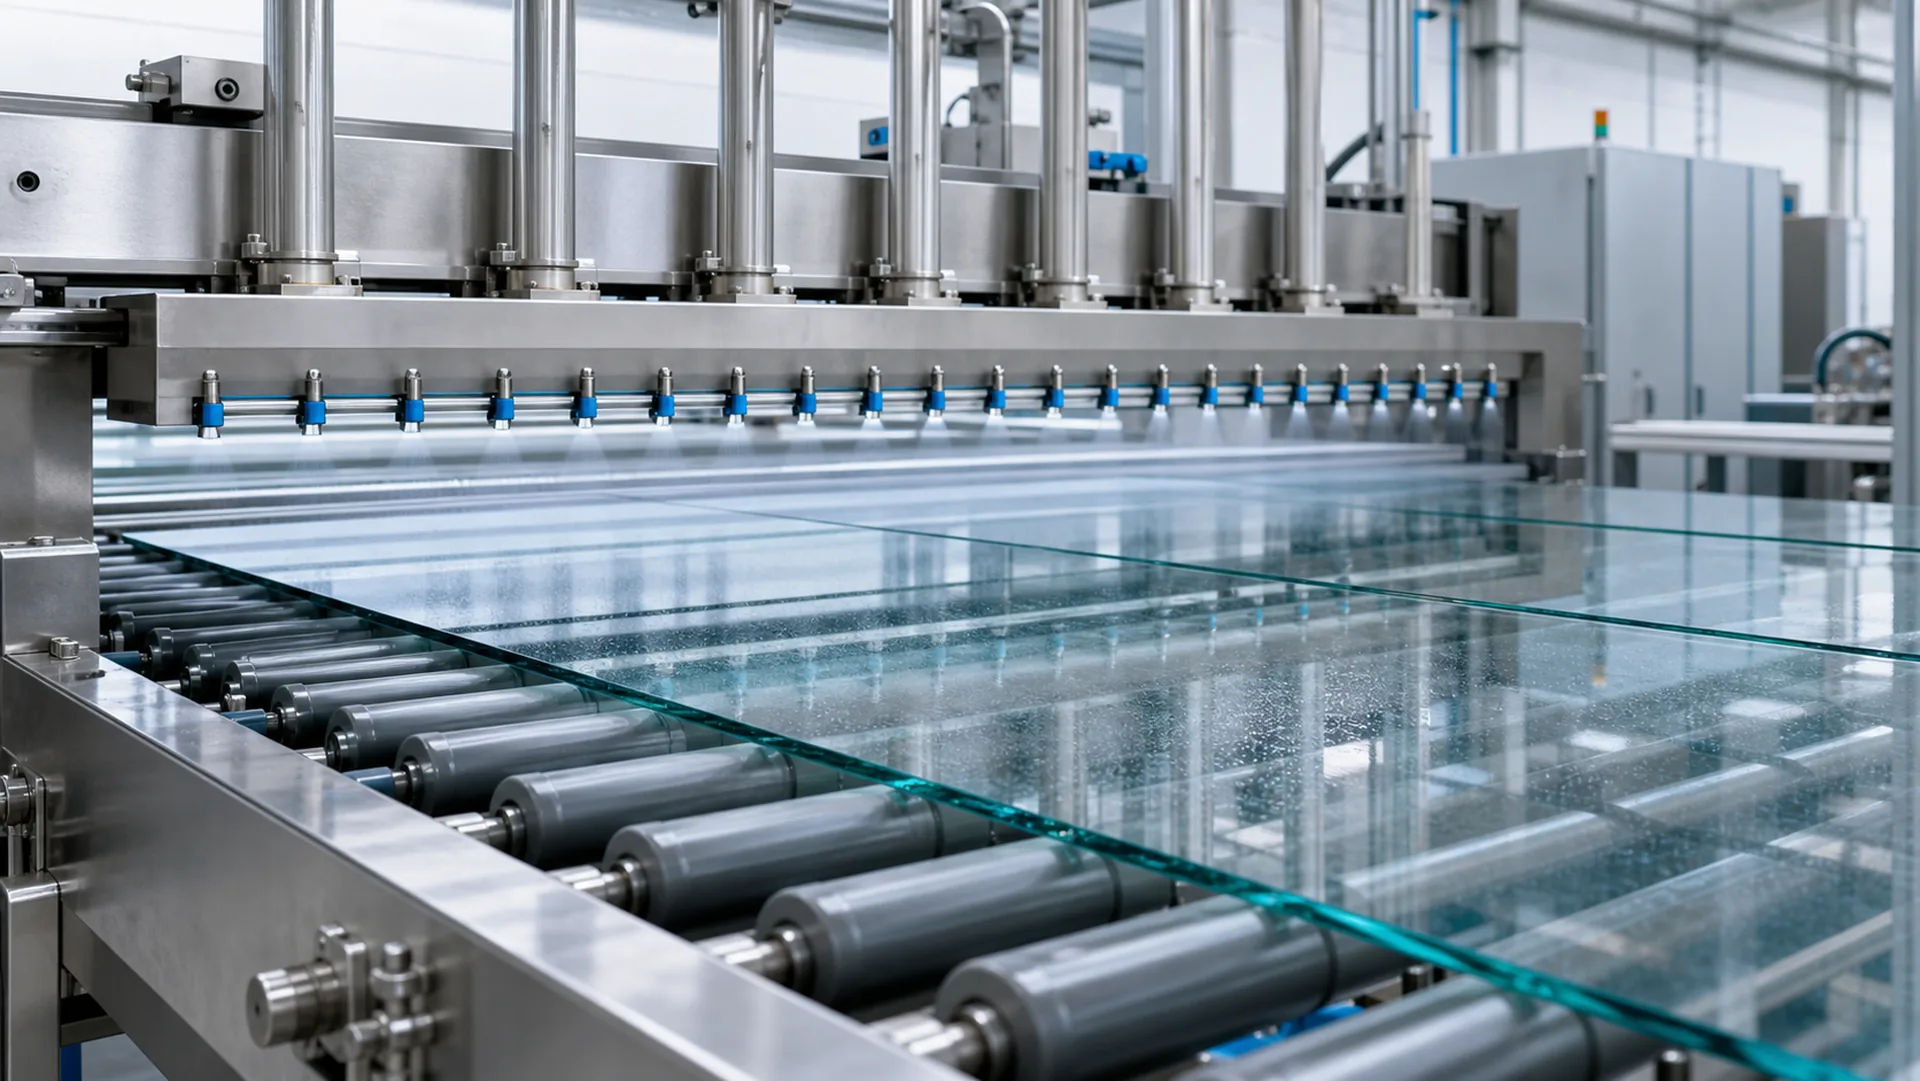
A glass sheet can leave a washer with a wet edge even when its center is dry. Another sheet may show a repeating line near a roller contact point or a band that stays at one machine position across several glass widths. These patterns provide better diagnostic evidence than a general request for more blower pressure.
This guide is a troubleshooting sequence for existing glass washing and drying lines. It does not replace a complete machine risk assessment, air-system design or model-specific blower selection review.
Map the wet area before changing a setting
Inspect representative glass at the dryer exit and again at the downstream quality point. Mark whether the remaining water is on the upper face, lower face, leading edge, trailing edge, corner or a fixed cross-line band. Record glass size, conveyor speed, washer recipe and the inspection method.
Does the mark follow the glass or stay on the machine?
A wet lower edge that follows each sheet suggests drainage or water carryover. A band that stays at the same cross-line position suggests a local air-knife slot, manifold or branch issue. Repeated marks that match roller spacing suggest shielding or water transfer. Treat each pattern as a testable clue rather than a final diagnosis.
Photographs and a simple wet-area map make it easier to compare trials. Inspect both faces because the visible downstream defect may originate on the opposite face.
Check the water load entering the drying section
Observe the final rinse and washer exit under the condition that produces the defect. Heavy water on one face, pooling at an edge or water carried by a roller can exceed the expected local drying load. Check whether rinse flow, spray alignment, roller condition, chemistry or drainage changed before the problem appeared.
A dry surface with a spot or haze may be a residue or water-quality issue rather than remaining liquid. Increasing air velocity does not correct rinse chemistry or contamination. Ask the washer or process owner to distinguish a wet defect from a surface-quality defect.
Compare the defect with air-knife coverage
Check the useful width and position of the upper and lower air knives against the actual glass range. Record nozzle angle, distance, overlap and any approved reference marks. A shifted knife, damaged edge or partially blocked slot can leave an untreated band even when the blower is supplying air.
If only one glass width fails, compare that edge path with the useful air zone. If different glass sizes show a mark at one machine position, inspect the local slot and its branch supply. Do not assume that higher total pressure will close a coverage gap.
Changes must remain within the equipment builder's limits for glass stability, guarding and surface protection. Adjust one approved variable at a time so the result can be interpreted.
Investigate rollers, guides and water transfer
Rollers and guides may shield a narrow area from useful air or transfer water back to the glass after the air knife. Compare the mark position and spacing with roller contact points. Inspect roller surfaces, alignment and water paths using the site's safe maintenance procedure.
Observe whether a sheet appears dry immediately after the knife but becomes wet again after the next roller. The correction may involve roller condition or drainage rather than blower capacity.
Trace drainage, splash and mist return
Water displaced by an air knife must leave the enclosure. Check for pooled water below the conveyor, restricted drains, splash from lower surfaces and mist moving back into the product path. A lower air knife can remove water effectively while also directing splash toward a later contact point if drainage is poor.
Enclosure exhaust can change the local air path. Coordinate exhaust or guard changes with the equipment owner; do not assume that more extraction or pressure will improve the pattern without a controlled observation.
Verify the air path without relying on motor power
Inspect filters, flexible connections, valves, branches and visible leaks. Record pressure or airflow only when the measurement location, instrument and operating condition are known. A motor nameplate or blower speed command alone does not show how much useful air reaches the glass.
Compare both upper and lower branches if the line uses separate knives. A common-supply problem normally affects several zones, while a local branch or nozzle problem produces a more limited pattern.
Retest at the production condition
Use representative difficult glass sizes and the conveyor speed at which the defect occurs. Record a baseline, change one allowed variable and inspect the same locations again. A useful trial record includes:
- glass size and relevant surface specification;
- conveyor speed and washer recipe;
- incoming water pattern and roller condition;
- active air knives, nozzle positions and blower command;
- filter, drain and enclosure condition;
- wet-area map at dryer exit and downstream;
- measured pressure or airflow with location and method.
A slower demonstration can hide an exposure-time or water-transfer problem. Keep the accepted production-speed record as a maintenance baseline.
When should the blower duty be reviewed?
Review the installed operating point only after obvious coverage, roller, drainage and restriction issues have been checked. Send the blower supplier the wet-area evidence, glass range, line speed, nozzle and branch layout, existing blower data and labelled measurements.
The purpose of the review is to determine whether useful airflow and pressure are deficient at the process point. It is not to select a larger motor from the wet-edge symptom alone.
Frequently Asked Questions
Why does only the edge of the glass remain wet?
Water may collect at the edge, miss the useful air zone or return from a roller or drain path. Map the exact edge and check incoming water and nozzle coverage before changing blower output.
What does a wet band at the same machine position suggest?
It may indicate a local slot, manifold, branch or roller issue at that position. Compare several glass sizes and inspect the installed geometry before concluding that total airflow is insufficient.
Can higher blower pressure remove roller-shadow marks?
Not necessarily. A roller may shield the air or transfer water after drying. Compare the mark with roller contact and observe the water path first.
What information should be sent for technical support?
Send photographs or a wet-area map, glass range, line speed, washer-exit condition, roller and air-knife layout, approved settings and labelled pressure or airflow measurements if available.